Scalable chemistry, from kilolab to commercial — kilolab development, pilot-plant trial batches, then full-scale manufacturing.
We take a route from development scale to routine commercial supply — kilolab development, pilot-plant trial batches, then full-scale manufacturing — with process safety, analytical method transfer and documentation carried through as one continuous workstream.
Chemistry and analysis move together. A route arrives at the next scale with its analytical method, impurity profile and process safety assessment already attached — which is what makes a transfer land on the first attempt rather than the third.
Discuss Your Project arrow_forward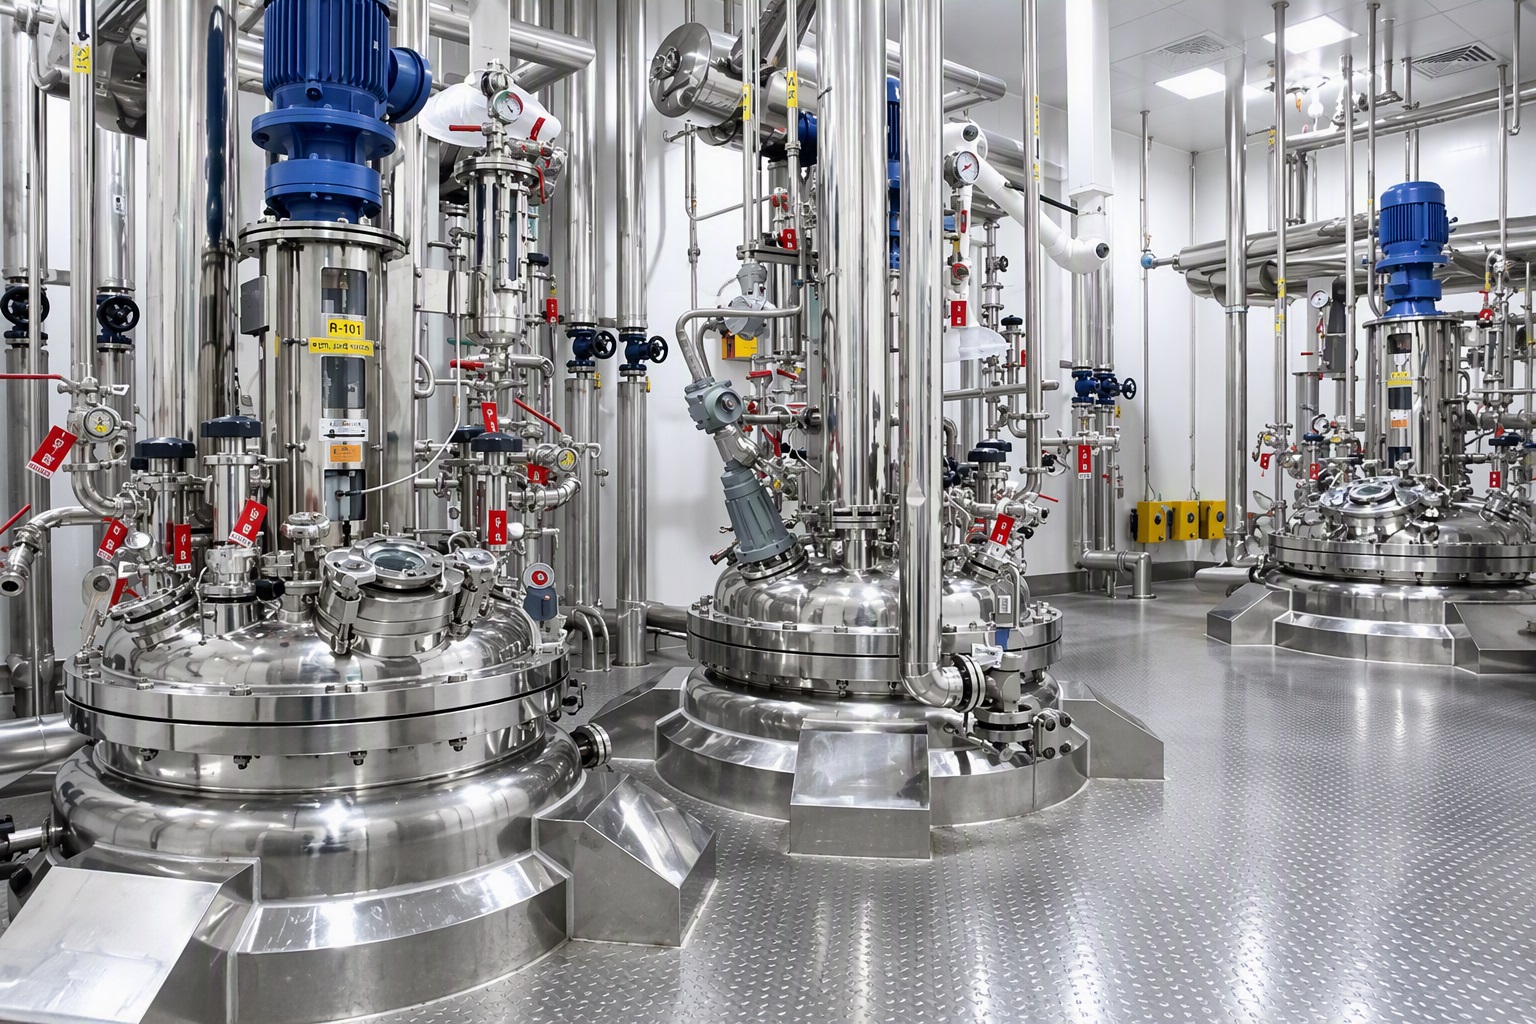
The route is established and de-risked at kilogram scale, confirmed at pilot scale, then run as routine commercial campaigns — with a fixed specification and complete documentation on every consignment.
The route is established at kilogram scale: reagent selection, work-up, isolation and the first honest look at the impurity profile. This is where a chemistry problem is still cheap to solve.
Trial batches at intermediate scale confirm that the chemistry survives real equipment — heat transfer, addition rates, hold times and filtration all behave differently outside a flask.
Full-scale campaigns against your schedule, with a fixed specification, batch-to-batch consistency and complete documentation — COA and MSDS on every consignment.
Each scale-up stage arrives with its analytical method, impurity profile and process safety assessment already attached — method transfer, process safety and documentation as one workstream.
| # | Stage | Purpose | Deliverable | Engagement | Next |
|---|---|---|---|---|---|
| 01 | Enquiry & Feasibility | Route assessment | Route map · quotation | Under NDA | Start → |
| 02 | Laboratory Development | Route establishment | Sample · draft specification | Development | Enquire → |
| 03 | Kilolab | De-risking at kg scale | Kilogram quantities · COA | Development | Enquire → |
| 04 | Pilot-Plant Trial Batches | Scale confirmation | Trial batch data · parameters | Development | Enquire → |
| 05 | Analytical Method Transfer | Method & impurity control | Validated method · impurity profile | Development | Enquire → |
| 06 | Commercial Manufacturing | Routine supply | Campaign batches · COA · MSDS | Commercial | Enquire → |
Adherence to Environmental, Health and Safety (EHS) standards, with defined chemical handling protocols applied to every reaction we scale. Hazards are assessed before scale, not after an incident.
Robust solvent recovery systems mean fresh solvent purchase is a design consideration in the route itself — not an afterthought once the chemistry is fixed.
Commitment to green chemistry principles, waste reduction and safe environmental practices — the difference between a route that can run for a decade and one that cannot.
Our Humnabad works runs one production block with a total installed reactor capacity of 110 KL — reactor bays, receivers, outdoor vessel lines, warehousing and the site itself. Individual vessel volumes and batch-size ranges are not published here yet.
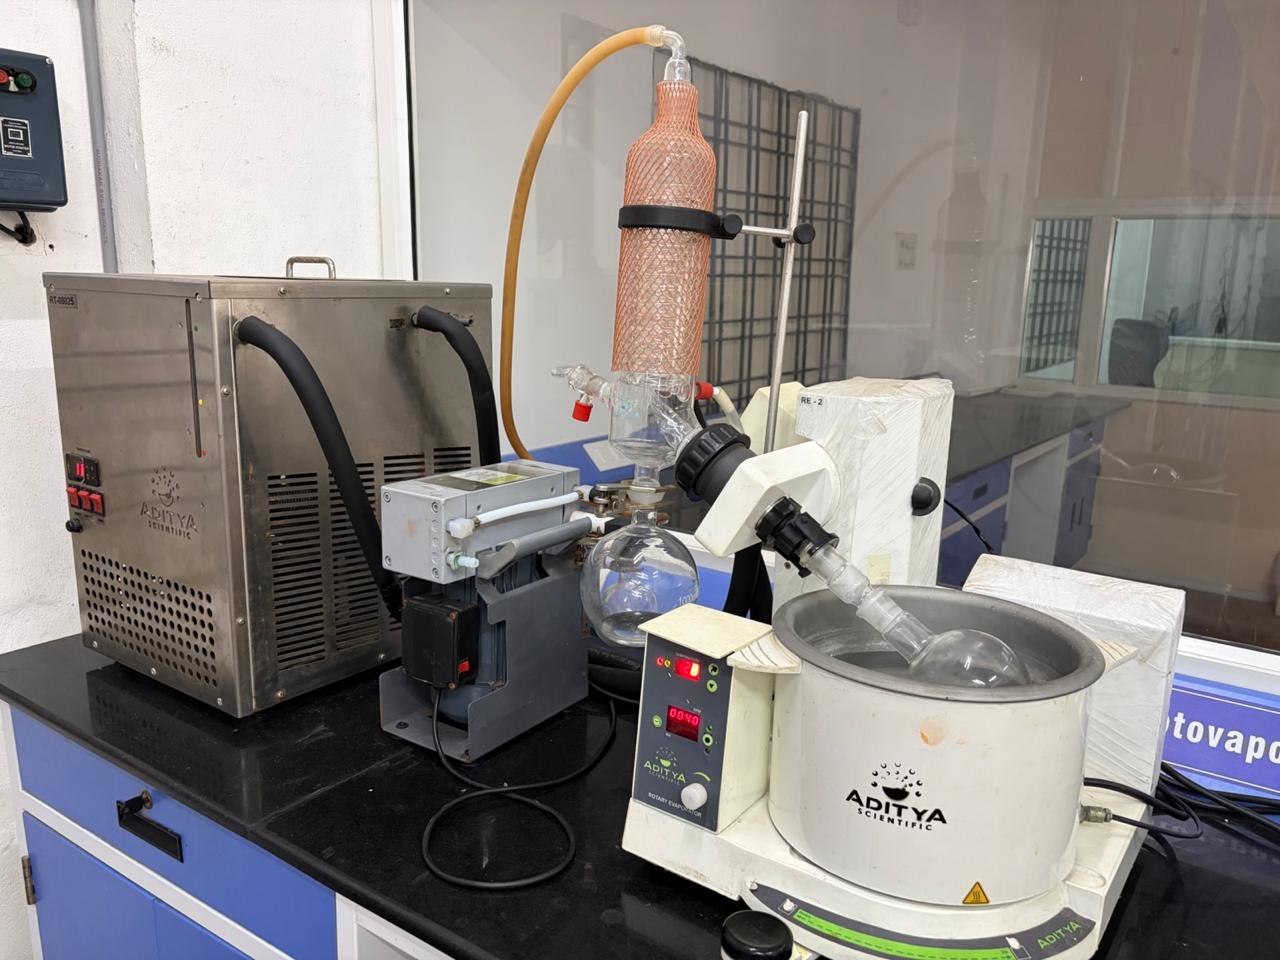
Route establishment · Balanagar
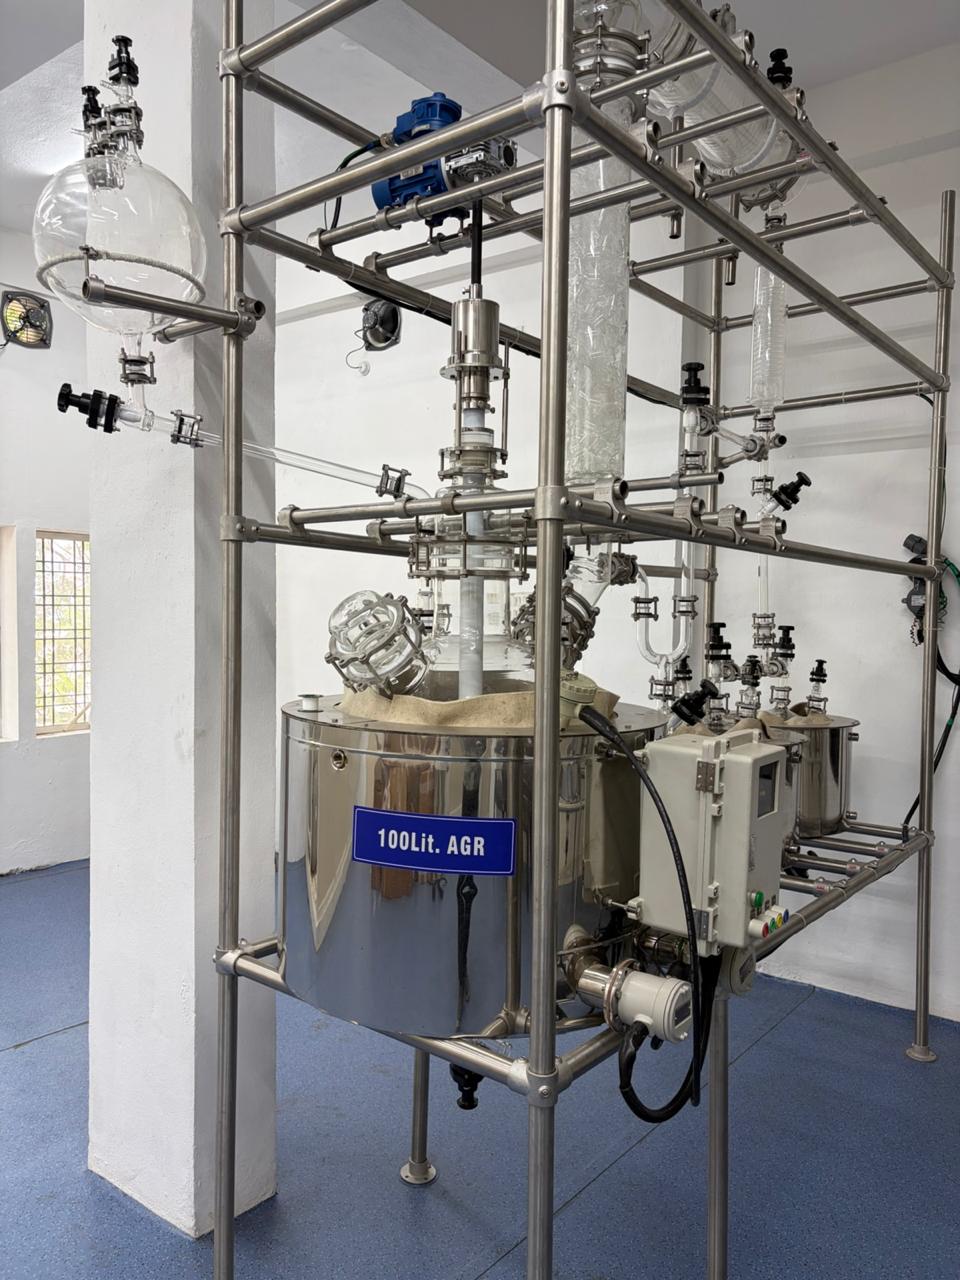
Method transfer · Balanagar
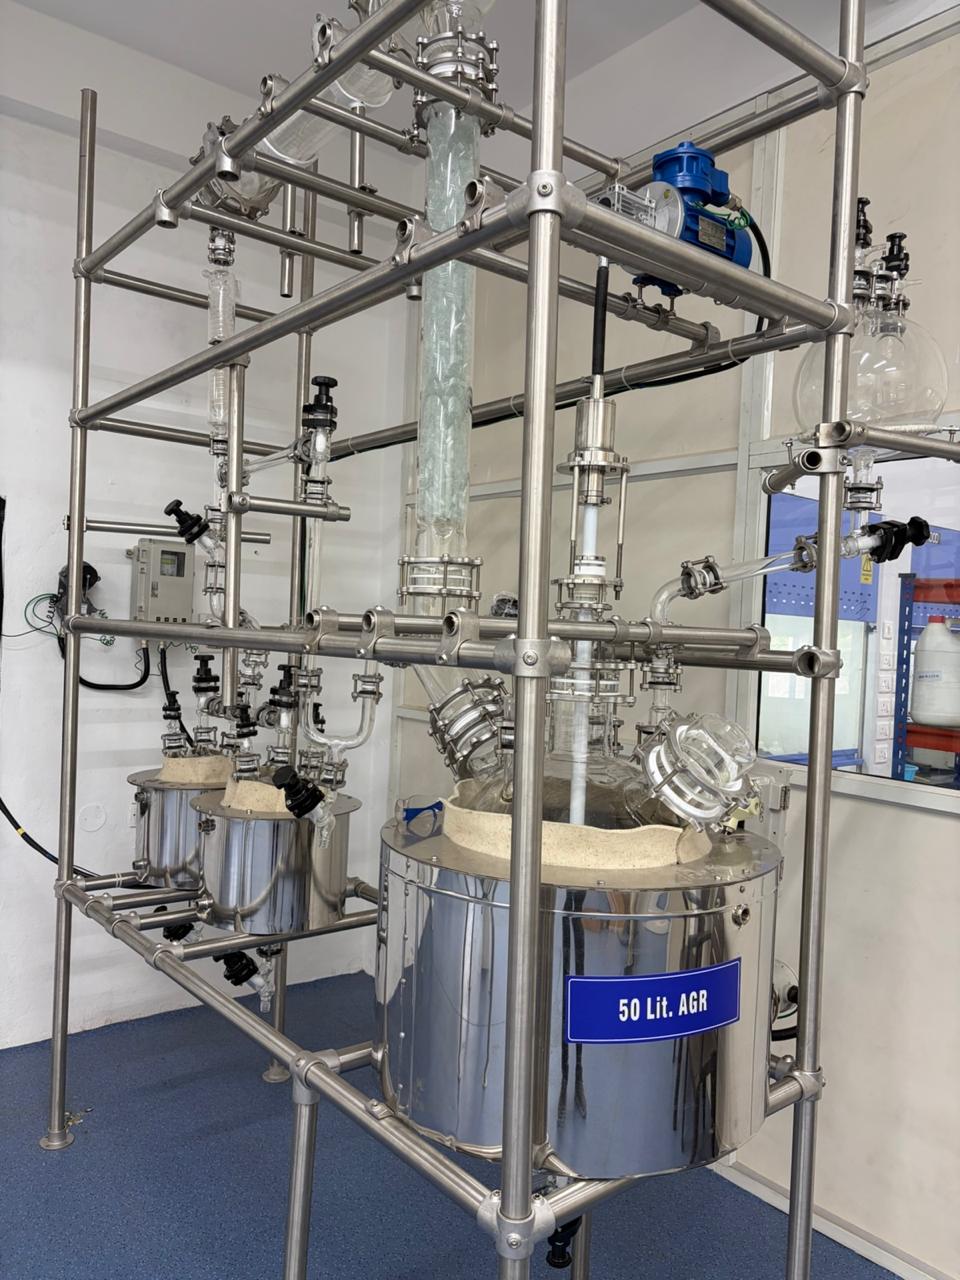
Impurity profiling · Balanagar
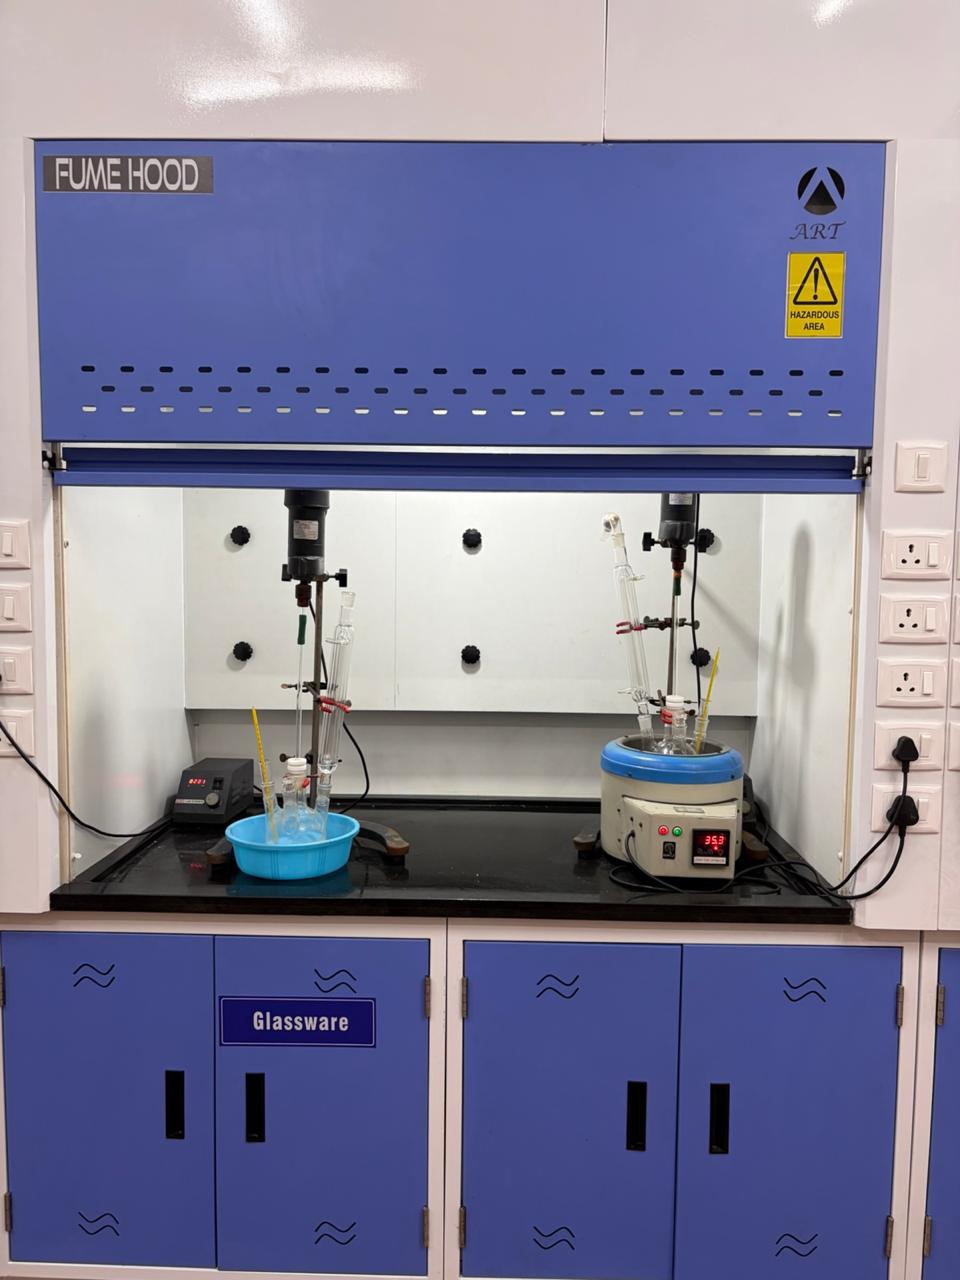
Trial batch support · Balanagar
Kilolab support · Balanagar
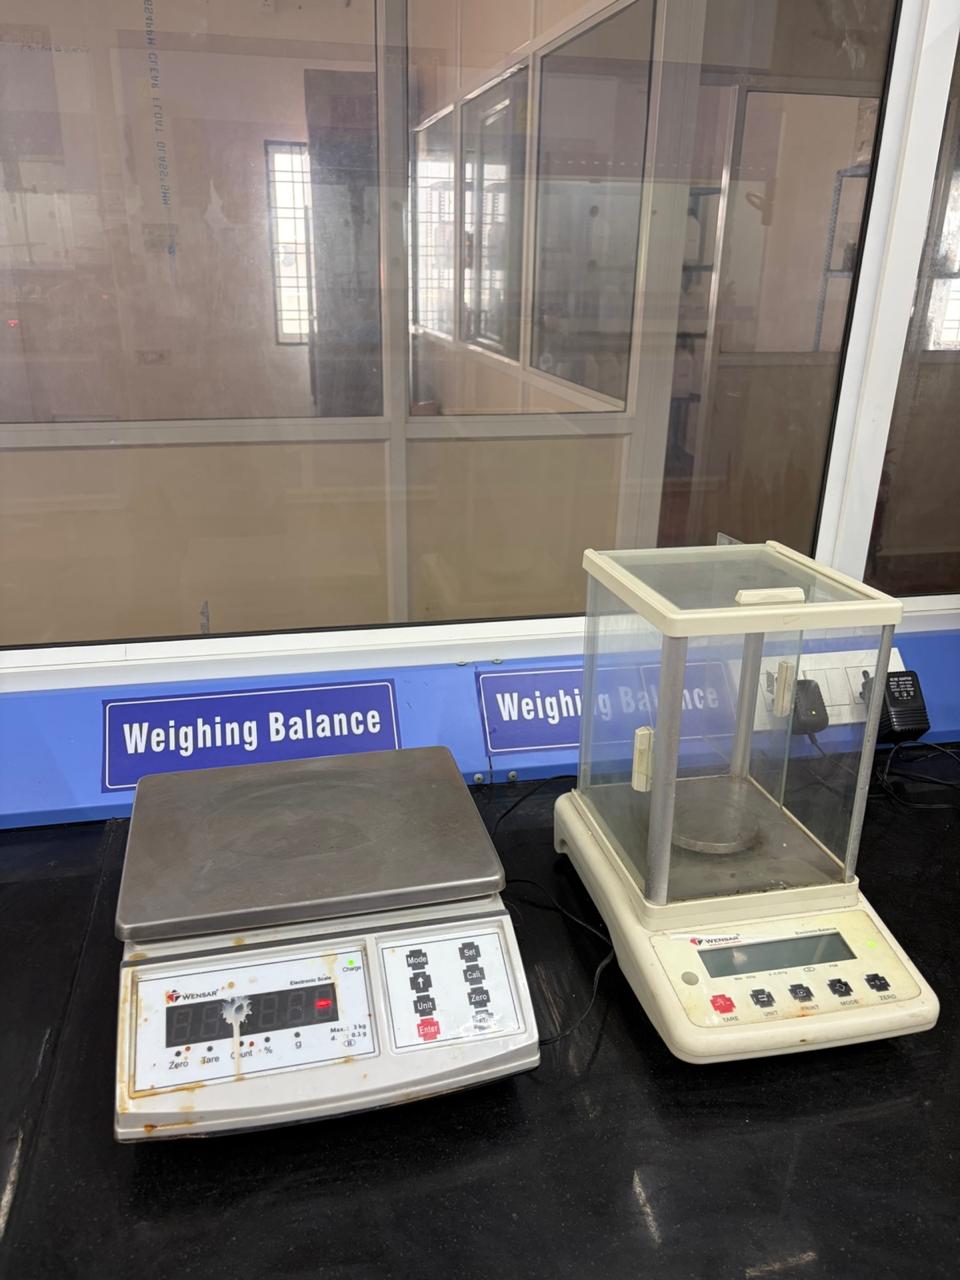
Balanagar, Hyderabad
Plant photographs of the Humnabad reactor bays and outdoor vessel lines will be published here as they are released. Laboratory photographs above are actual site images from Balanagar.
Partner with us for your development and manufacturing needs.
Contact Our Team